
Cable Tray Production Line
Patented Rotary Punch and Integrated Roll Forming Line
A fully integrated cable tray production machine and manufacturing line with continuous punching at about 1,400 metres per hour (24 m/min), running 4–6 times faster than conventional press lines.
Step-by-Step Production Method
The Cable Tray Production Line punches galvanised or black coil sheet without stopping it, straightens it, cuts it to length and roll-forms it into the final cable tray profile. Running 4–6 times faster than conventional press lines, it produces about 1,400 metres of perforated sheet per hour and can be run by a single operator.
Key Engineering Parameters
- Sheet feeding from a hydraulic mandrel uncoiler with 5-tonne capacity and sensor-controlled loop
- Punching at 24 m/min without stopping the sheet in the patented Rotary Punch unit
- Profile forming on a 16–18 station roll former after 9-roll straightening and guillotine cut-to-length
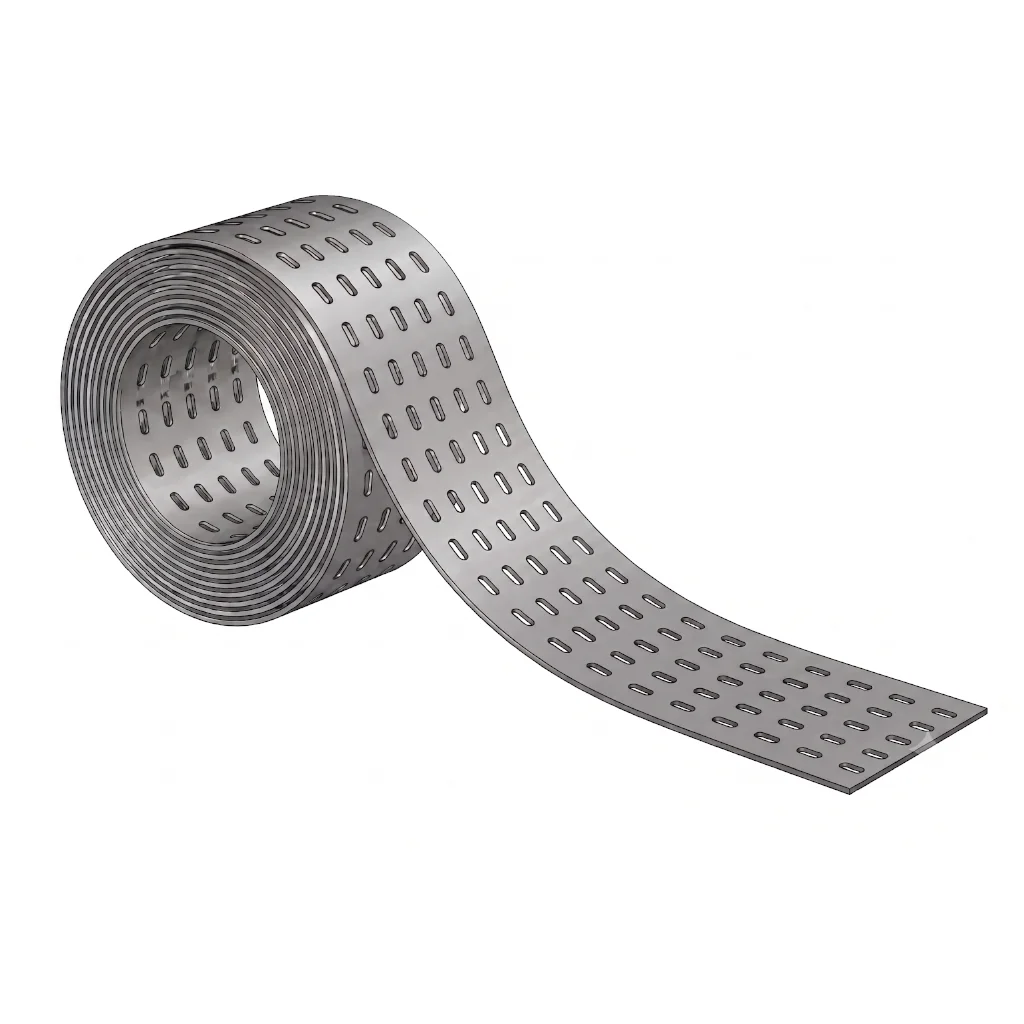
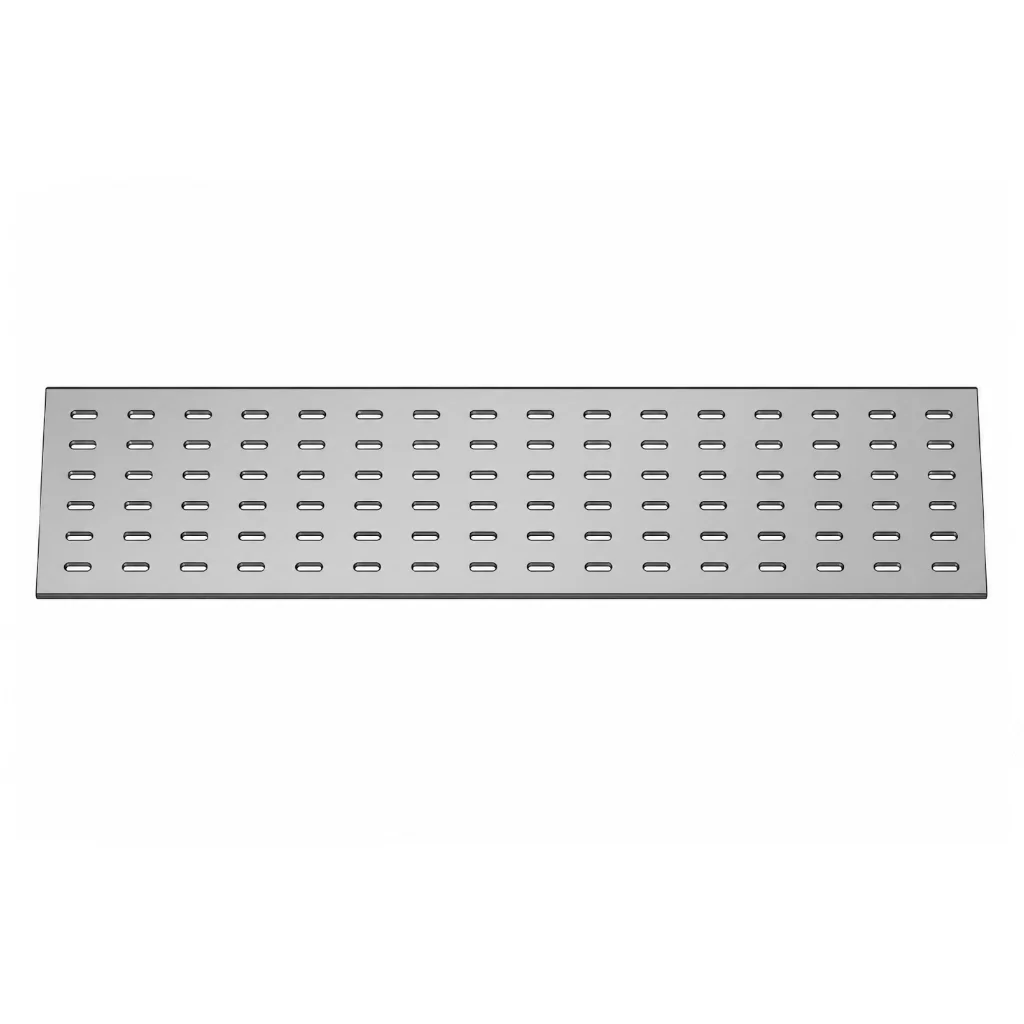
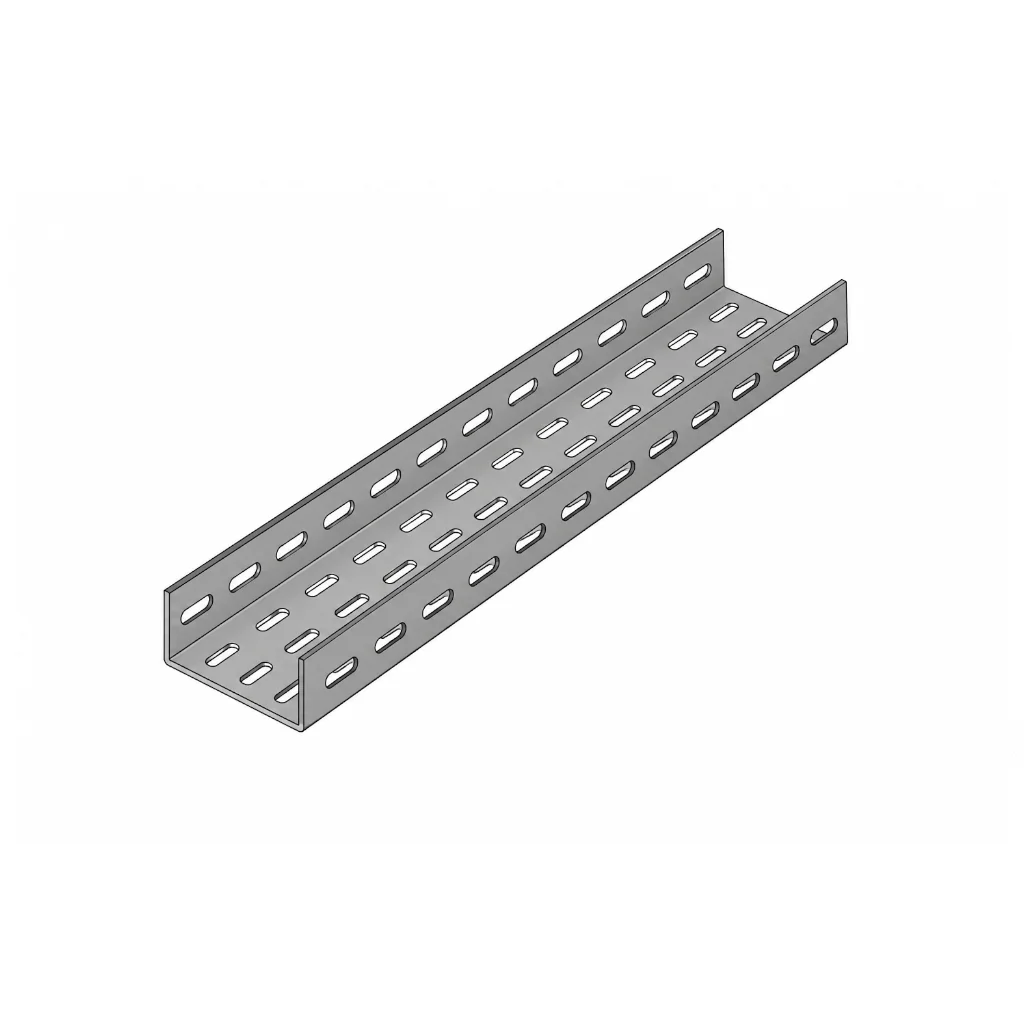
"Patented Rotary Punch punching at a non-stop 1,400 metres per hour and a roll forming system with stepless automatic NC width adjustment."
Uncoiler
Rotary Punch Punching
Straightener Feeder
Roll Forming
Engineering Architecture of the Cable Tray and Cable Support Systems Production Line
The YILSA Cable Tray Production Line is an integrated production system that turns pre-galvanised or black coil sheet into perforated cable tray at a non-stop speed of 24 metres per minute (about 1,400 metres per hour). The patented Rotary Punch punching unit, which eliminates the stop-and-go motion of conventional press lines, makes production 4–6 times faster and removes the need for an eccentric press of about 400 tonnes and complex dies.
The line produces tray widths from 50 mm to 600 mm (up to 1000 mm on special projects) and side heights from 40 mm to 100 mm. Size changes are made with a motorised NC adjustment system, without changing rollers.
Continuous Perforation & Rotary Punch Technology
Sheet from the uncoiler goes straight into the Rotary Punch drums. Punches rotating at the same speed as the sheet make 7×18 mm oval (R3.5) holes at 50 mm horizontal and 25 mm vertical spacing, at 24 metres per minute, without stopping the sheet. Hole edges are burr-free on pre-galvanised and black St37 sheet from 0.7 mm to 2.0 mm. The dies are made of 1.2379 (D2) tool steel hardened to 60 HRC.
Straightening, Guillotine Cut-to-Length & Roll Forming
The punched sheet is flattened in the 9-roll straightening and feeding unit and then cut to the required length by a hydraulic or eccentric guillotine shear. The cut length is set in multiples of 50 mm; the standard length is 2400 mm, and other lengths such as 2500 mm or 3000 mm can also be cut. The cut sheet is fed via the infeed conveyor into the 16–18 station roll forming machine and formed into a tray with surface-hardened C 4140 forming rolls without damaging the galvanised coating.
Automation, Energy & Efficiency
The line is controlled by a PLC and HMI. Rotary Punch technology uses 0.16–0.25 kWh of energy per metre (0.8–1.2 kWh/m on press lines) — up to 80% energy savings. The punching unit processes 11,520 metres of sheet in an 8-hour shift, and the roll forming line produces 4–6 tonnes of tray per day. Installed in an area of about 30 × 3 × 3 m, the line can be run by a single operator and is CE certified. It produces heavy-duty and standard-duty perforated cable trays; delivery time is 8–10 months.
Machines in the Line
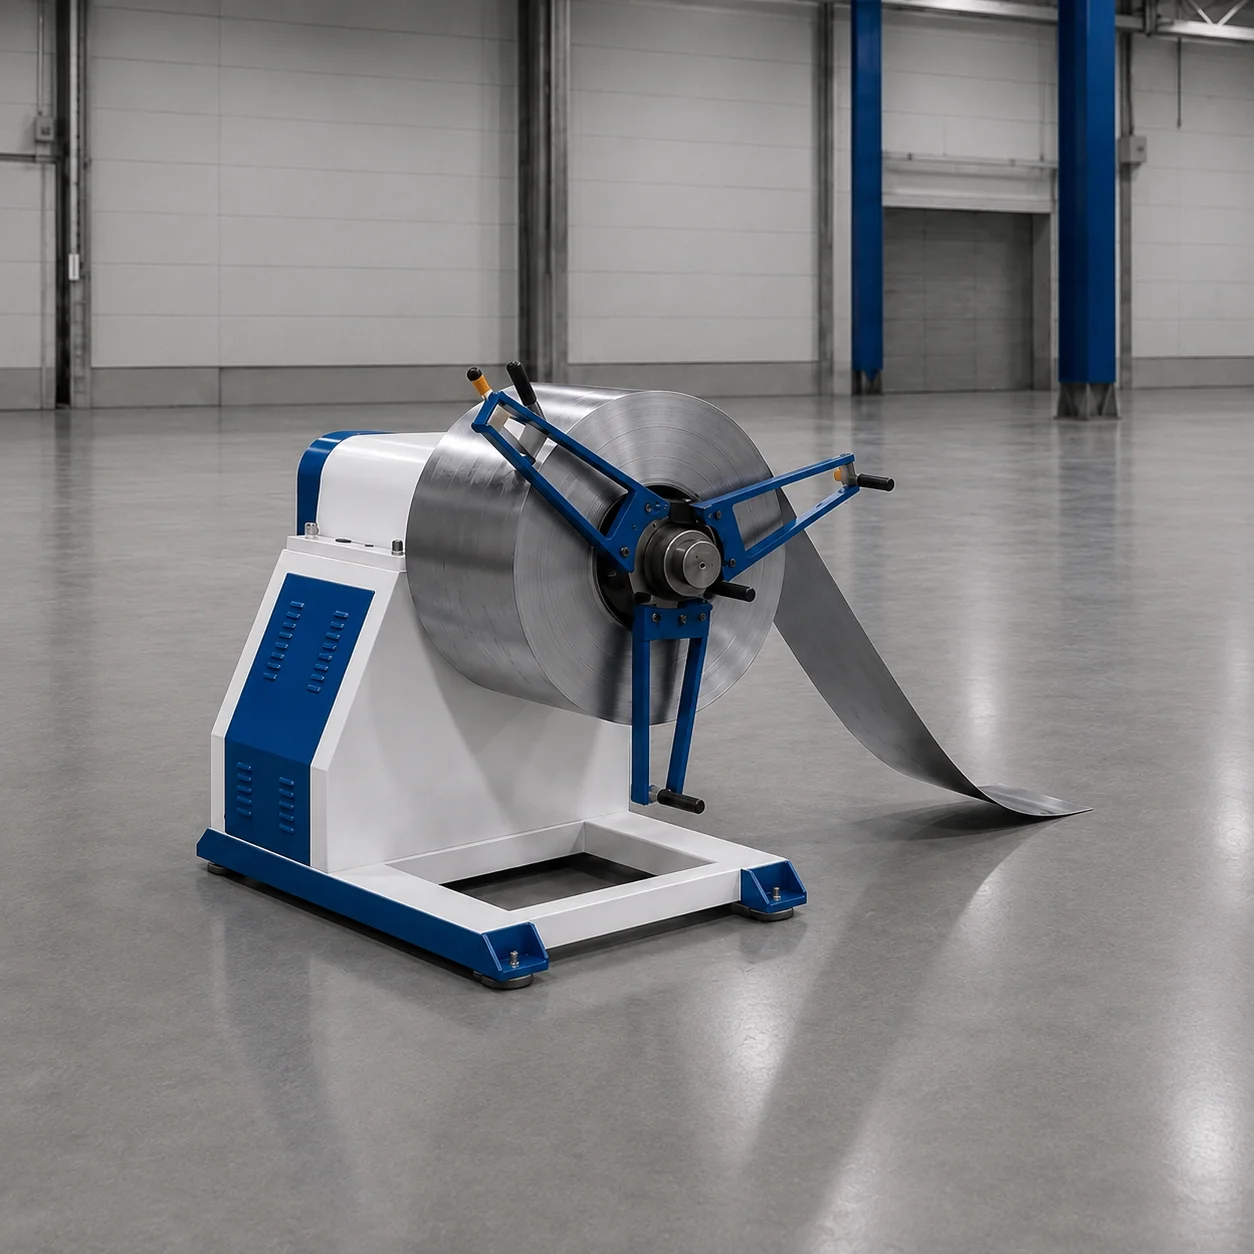
Uncoiler
Mechanical and Hydraulic Uncoiler Machine for Coil Sheet
YILSA uncoilers (decoilers) are built in capacities from 300 kg to 10 tonnes, with a choice of coil widths and inner/outer diameters; in mechanical and hydraulic versions they feed any sheet coil into the production line in a controlled way.
This line uses the 5,000 kg model with sensor-controlled loop.
Rotary Punch Punching
Patented Rotary Punch Continuous Sheet Punching Unit
With punch drums rotating at the same speed as the sheet, it punches coil sheet at 24 m/min without ever stopping it. Unlike eccentric presses, production is impact-free and burr-free.
Straightener Feeder
Sheet Straightening and Feeding Unit
A unit that flattens sheet from the uncoiler with straightening rolls and feeds it with pinch rolls, in sync, to the next unit of the line (press, guillotine, roll former); built in different widths and thicknesses to suit the line.
This line uses the 9-roll model with guillotine shear; the sheet is cut to length before roll forming.

Roll Forming
16–18 Station Roll Forming Machine (Roll Forming Profile Line)
With 16–18 stations of forming rolls, it shapes the cut-to-length perforated sheet step by step into a cable tray without strain. Its motorised NC system changes size without changing rollers.