
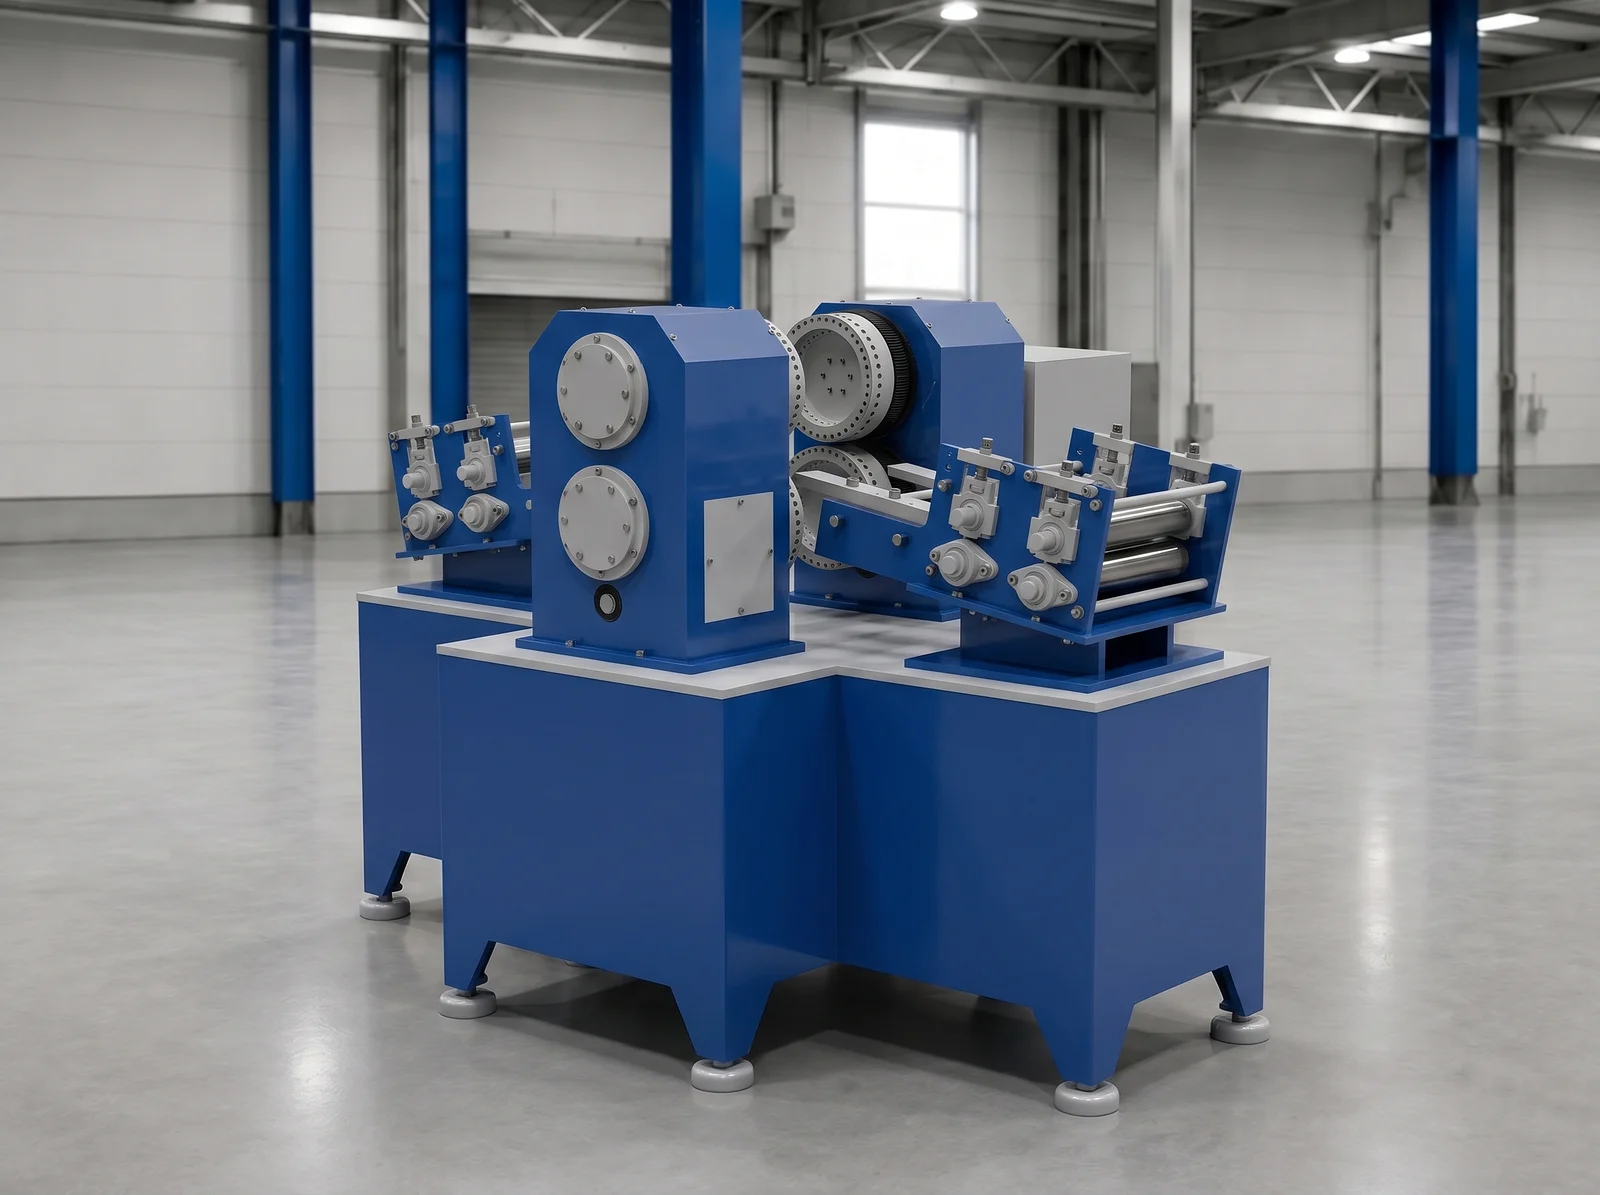
Omega Ventilation Profile Machine
Omega Ventilation Profile Punching Machine with Rotary Punch
Punches the hole pattern of ventilated omega profiles in the flat sheet strip before bending, non-stop, with synchronised male and female die drums.
Continuous Punching of Omega Profiles Before Bending
Ventilated omega profiles are made with a regular hole pattern for airflow in construction and industrial applications. The machine punches this pattern in the flat sheet strip before the profile is bent.
Synchronised Male and Female Die Drums
In YILSA's patented Rotary Punch technique, the drums carrying the male and female dies rotate at the same speed as the sheet, and the holes are punched as the sheet flows. Because the sheet is not stopped, punching speeds of up to 17 m/min are reached.
Because the drum position is adjustable, different unformed sheet widths from 143 to 253 mm can be processed on the same machine.
Dual Drive and Smart Control
The machine is driven by 2.2 kW, 0.75 kW and 0.75 kW AC motors via speed control units. The dual-drive design keeps the sheet flowing smoothly between the drums.
Operation is automatic or manual via the HMI touch screen, with built-in fault diagnosis, error log and maintenance tracking.
Easy Maintenance
The dies are made of 1.2379 (D2) tool steel at 58–60 HRC and removed one by one via set screws. Thanks to the 6 mm regrinding allowance on the male and female dies, the height of a resharpened die is easy to reset.
The machine measures 2 × 1.5 × 1.5 m and weighs about 1.7 tonnes.
Technological Advantages & Innovation
- The hole pattern is punched in the flat strip before bending, without stopping the sheet
- Synchronised male and female die drums; burr-free, regular hole pattern
- Adjustable drum position for unformed sheet widths of 143–253 mm
- 6 mm regrinding allowance on male and female dies; dies are easily removed via set screws
- HMI touch screen, automatic and manual operation, fault diagnosis and error log
Custom Engineering
We build custom-engineered machines for your specific size and technical parameter requirements.